

Chamfering
Chamfering cuts the end of a stud or bolt back at an angle, from the outside of the thread to its root diameter or below, so a nut starts cleanly on a full thread. A sawn end has a burr and a ragged start to the thread, and the ASTM bolting specifications require ends to be flat and chamfered, or rounded.
Cut, chamfer, check, mark.
- STEP 01
Cut to length
Studs are sawn from threaded bar, or turned and threaded from a blank. Length is measured from first thread to first thread, so the points are extra (ASTM A962).
- STEP 02
Chamfer
On the chamfering machine the stud is clamped in a vise against a stop, and a spinning cutter head with carbide inserts feeds onto the end, taking it down at 45° from the major diameter to the root diameter or below and removing the burr and the ragged start of the thread. The stud is then turned end for end by hand and the other end chamfered.
- STEP 03
Face
The end is left flat and square to the axis, with room for the grade and maker's marks.
- STEP 04
Check the point
A NOT GO ring on the major diameter shows where the full thread starts. The chamfered length must be one to two pitches (ASME B18.31.2): 0.125 to 0.250 in. on a 1 in.-8 stud.
- STEP 05
Mark
Grade and maker's symbols go on one end of studs 3/8 in. (10 mm) and larger (ASTM A962).
- A rounded end may be used instead of a chamfer at the maker's choice (ASTM A962, A193); the one-to-two-thread rule still applies.
- A 45° chamfer at the start of a cut thread keeps the threading from leaving a burr; rolled threads form their own lead-in of about 45°.
- Nuts are double chamfered or washer-faced instead, with the tapped hole countersunk at the face.
The first thread is where the nut starts, or doesn't.
A saw cut leaves a burr and a ragged thread start that make a nut hard to start straight. Chamfering to below the root removes both, so the nut meets a clean, full thread first.
It is a requirement, not a nicety. ASTM A962, which A193, A194 and A320 call up, has studs and bolts pointed, flat and chamfered or rounded, with the point one to two complete threads long. ASME B18.31.2 sets the chamfered length, U, for every stud size.
Done in-house, chamfering follows the saw in the same job, so studs cut to odd lengths from certified threaded bar ship finished, marked and paired with their nuts.
Parts and features.
Chamfering: common questions.
How long is the chamfer on a stud?
One to two thread pitches, to the first full thread: 0.077 to 0.154 in. on a 1/2 in.-13 stud, and 0.125 to 0.250 in. on a 1 in.-8 stud or any 8-pitch stud (ASME B18.31.2).
Is a rounded end acceptable?
Yes. ASTM A962 and A193 let the maker choose flat and chamfered, or rounded; the point is still one to two threads long.
Does the chamfer count in the stud length?
No. Stud and stud bolt length is measured from first thread to first thread (ASTM A962), so the points lie beyond the ordered length.
Why chamfer before cutting a thread?
A 45° chamfer at the start of a cut thread stops the tool or die leaving a burr there. Rolled threads form their own lead-in, close to 45°.
Before and after it.
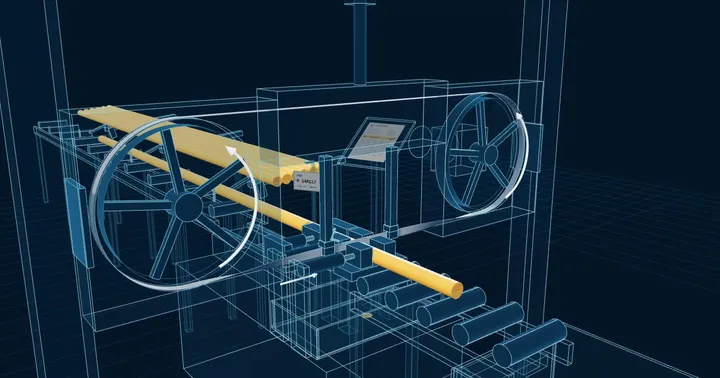
Band sawing
Certified bar cut to length, heat kept
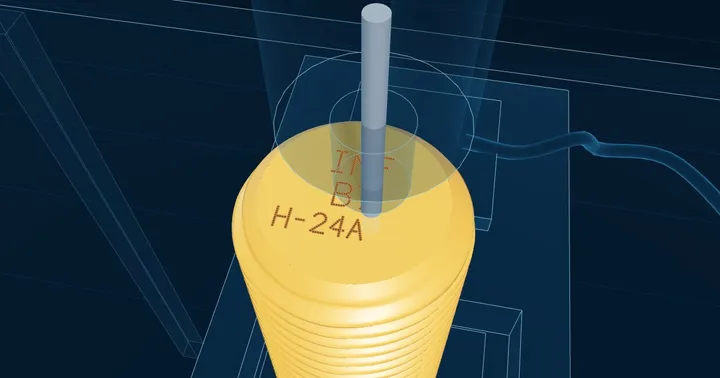
Dot-peen marking
Grade, maker and heat marked into the part, dot by dot
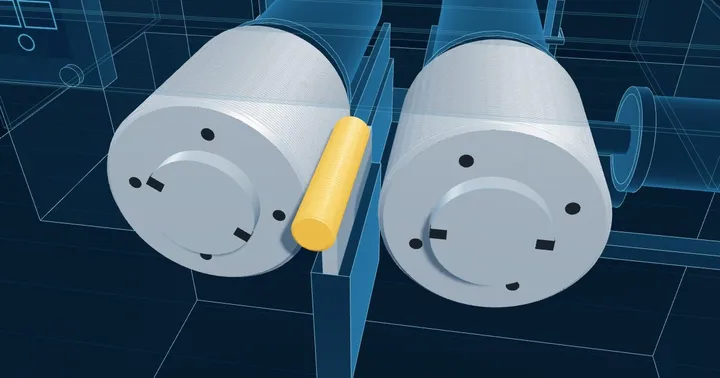
Thread rolling
Threads pressed into the bar, not cut out of it
Thread gauging and dimensional inspection
Threads are checked with Go and No-Go ring and plug gauges, and pitch diameter is measured by the three-wire method or on a thread comparator. Heads, flats, lengths and radii are measured with calibrated instruments and, for complex parts, on the CMM.