

Tapping nuts
A nut's thread is cut by a tap, a hardened threaded tool that advances exactly one thread pitch for every turn as it cuts. We tap nuts to Class 2B or 3B, and tap nuts for hot-dip galvanized bolts oversize after galvanizing, as ASTM A563 requires.
Bore, tap, gauge.
- STEP 01
Make the blank
The nut is turned from bar or forged, its faces chamfered or washer-faced, and bored or drilled to the thread's minor diameter.
- STEP 02
Size the hole
The hole sets the minor diameter, which ASME B1.1 limits for each size and class: 0.417 to 0.434 in. for a 1/2 in.-13 Class 2B nut.
- STEP 03
Tap
The tap turns into the hole and advances one pitch per turn while its tapered lead cuts the thread. A spiral-point tap pushes the chips ahead and out through the nut.
- STEP 04
Clear the tap
The tap reverses and backs out along the thread it cut, or passes clear through the nut.
- STEP 05
Gauge
A GO thread plug must run through; the NOT GO plug must not enter beyond the start the gauging standard allows (ASME B1.2).
- Large or special internal threads that a standard tap does not suit can be single-pointed on a lathe instead.
- Very large runs of standard nuts are tapped on continuous bent-shank tappers, which feed nut after nut onto the tap.
- Nuts for mechanically zinc-coated or zinc-flake-coated bolts are tapped oversize before coating, not after (ASTM A563).
The nut has to fit the bolt it will meet.
Nut threads have no allowance: at its minimum a Class 2B or 3B thread is at basic size, so there is no room in it for a coating on the bolt. Class 2B is the default for ASTM A194 and A563 nuts; 3B holds a closer tolerance where the drawing calls for it.
Hot-dip zinc is far too thick to fit, so ASTM A563 has nuts for galvanized bolts tapped oversize after galvanizing, by a set allowance: 0.018 in. on a 1/2 in.-13 nut, 0.024 in. on 1 in.-8, 0.050 in. from 1-3/4 in. up. The bolt is threaded to the normal Class 2A before it is galvanized, and the zinc on its thread protects the bare thread of the nut. Overtapped nuts are proof load tested after galvanizing and tapping.
A194 nuts follow the same rules when galvanized: a zinc-coated 2H nut supplied for A563 work is overtapped and lubricated to A563, and A194's coated-nut marking puts ZN after the grade, as in 2HZN. Overtapping takes away thread depth, which A194 warns can cost load capacity, and A563 lists 8-pitch allowances only up to 1-1/2 in.
Parts and features.
Tapping nuts: common questions.
2B or 3B?
2B is the standard class for nuts and the default in ASTM A194 and A563. 3B holds a closer tolerance; order it when the drawing or the mating part calls for it. Neither has an allowance, so neither leaves room for a coating.
Why are galvanized nuts tapped after galvanizing?
So the tap clears the zinc out of the thread and cuts the oversize thread in clean steel; a nut tapped first comes back with zinc in its thread. ASTM A563 requires hot-dip galvanized nuts to be overtapped after coating, and the zinc on the bolt then protects the bare nut thread.
Will a zinc-plated nut fit a galvanized bolt?
No. Plated nuts are tapped to the normal size, and the galvanized bolt thread is too full to enter. Order nuts overtapped for galvanizing and coated by the same process as the bolts (ASTM A563).
Before and after it.
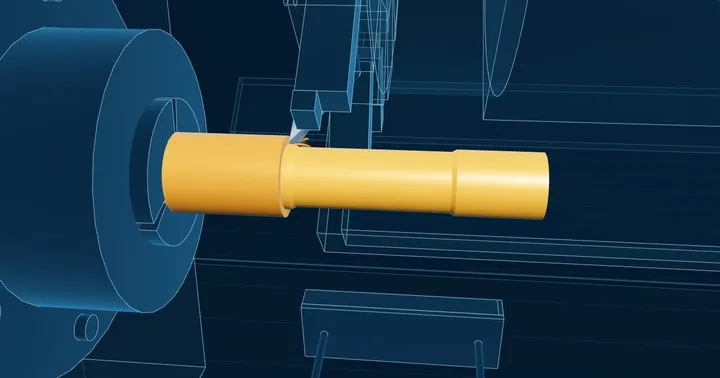
CNC turning
Studs, collars, nuts and parts from bar
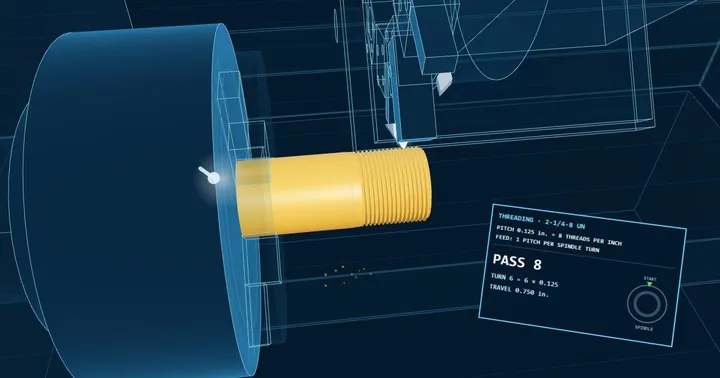
Single-point threading
One insert, many passes: any size or form on a CNC lathe
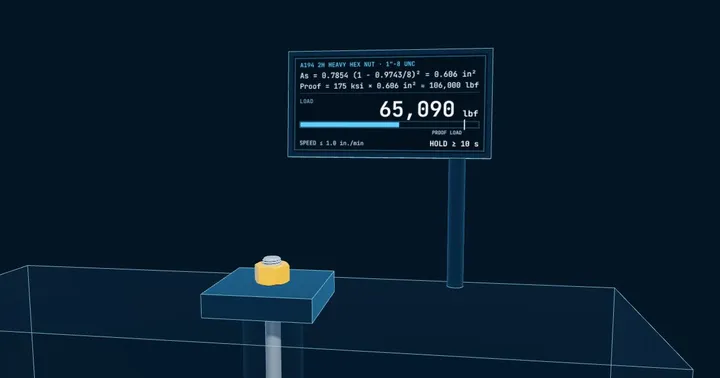
Proof load testing of nuts
The nut is threaded on a hardened mandrel and loaded to the proof stress for its grade and size. It passes if the threads neither strip nor break and it can be removed by hand afterwards; a wrench may start it, for up to half a turn.
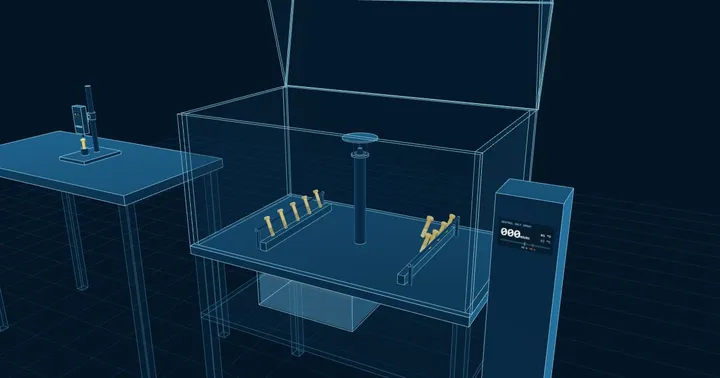
Coating thickness and salt spray
Coating thickness is measured with a magnetic or eddy-current gauge, or by X-ray fluorescence for thin platings, and checked against the class ordered. Salt-spray exposure checks corrosion protection on a sample from the lot when the specification calls for it.