

Custom Fasteners Made to Drawing, Fast — Houston, 24/7
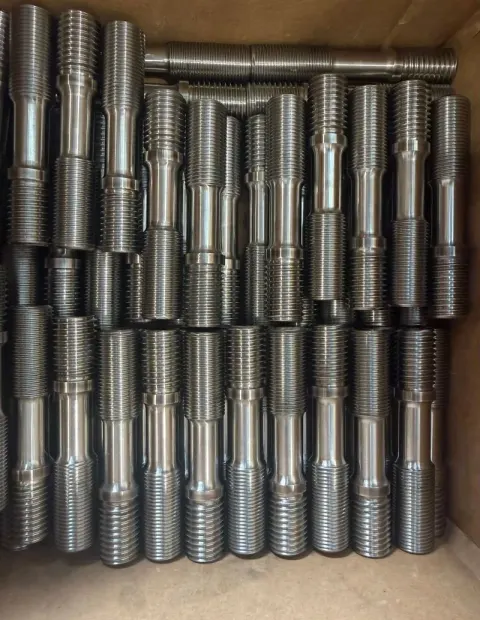
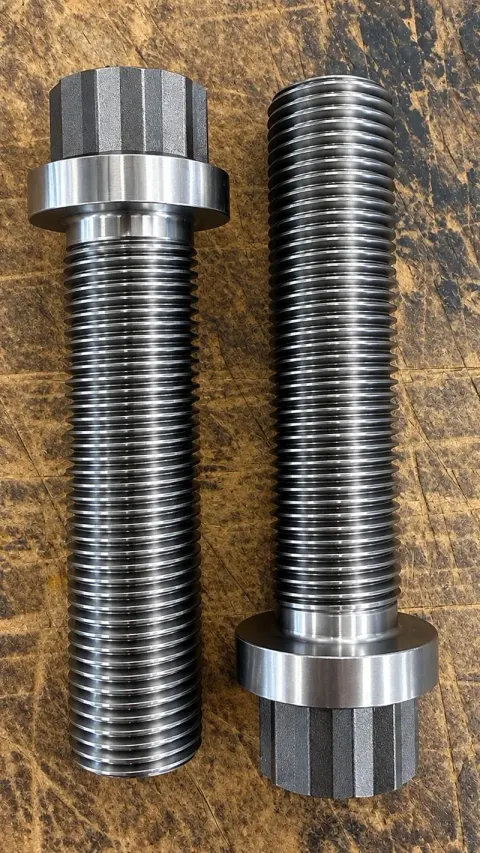
When the part is not a catalog item — a stud with two different threads, a 12-point flange bolt, a tee-head bolt, a one-piece stay rod, a casing cap nut or a machined pin — we make it to your drawing or from a sample, in our Houston shop, in the alloy steel, stainless, duplex, nickel and copper alloys on our materials pages. Send a drawing, a spec, or the part that failed. Every quote goes back within 24 to 48 hours; for an emergency, call 832-446-3442, answered 24/7.
We saw, turn, mill, thread (rolled, die-head cut or single-point), broach sockets, forge heads and mark parts under one roof, so a special does not wait in another shop's queue. Only heat treatment and coating go out, to approved Houston processors.
Parts we make to your drawing or sample.
| Part | Made for |
|---|---|
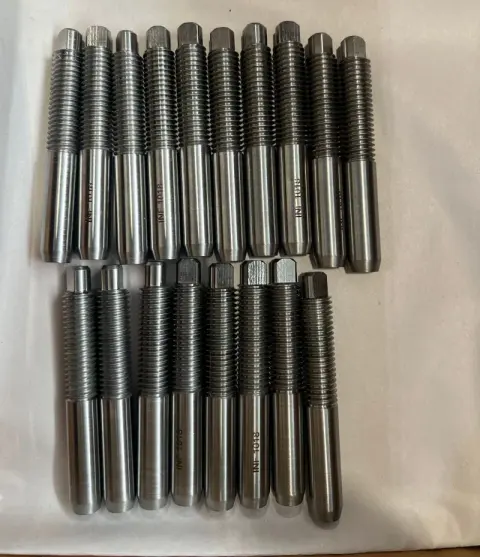
| Custom studs | Dissimilar threads, reduced shanks, collars, odd lengths. |
| Custom bolts & screws | Special heads and geometries, special materials. |
| 12-point flange bolts | Integral flange, 12-point head for tight spaces. |
| Turbine studs | To the turbine OEM drawing. |
| Stay rods | Frac pump stay rods, one- and two-piece, with sleeves and nuts. |
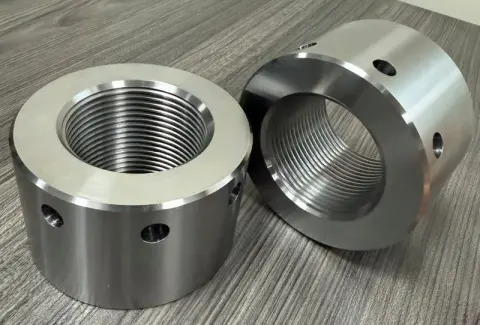
| Casing cap nuts | Round body and closed top turned from bar. |
| Custom nuts | Special heights, threads and shapes. |
| Custom socket screws | Stainless and nickel-alloy sockets broached in-house. |
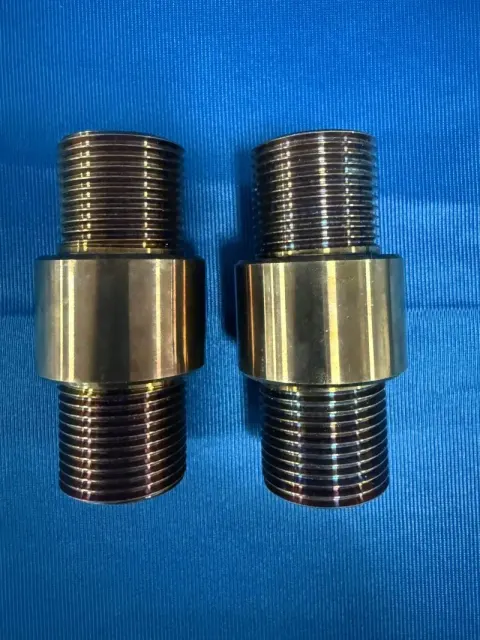
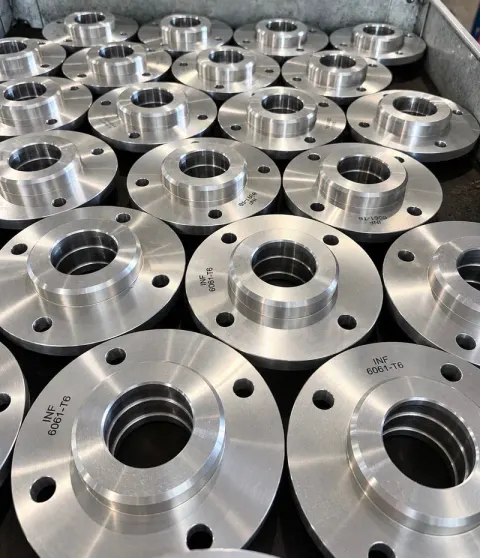
| Machined components | Pins, sleeves, plugs and adapters to print. |
| Tee-head bolts | Made to drawing for waterworks. |
| Rock bolts & ground anchors | Made to drawing for mining ground support. |
Where these parts go.
- Replacing an obsolete or one-off OEM part on equipment that is down.
- Turbine, pump, compressor and valve overhauls.
- Frac fleet stay rods and fluid-end bolting.
- Waterworks tee-head bolts and mining ground support.
- Short runs for equipment builders.
So we can start on the call.
- A drawing — PDF, DWG, DXF or STEP — or the spec and a sketch.
- Or the part that failed. We confirm dimensions, threads and grade with you before we cut metal.
- Grade and specification, quantity, and the date you need it.
- Coating, marking and certification requirements.
One shop, from bar to box.
- Sawing, turning, milling, threading, socket broaching, forging and marking are all done in-house.
- Only heat treatment and coating go to outside Houston processors.
- A drawing with tolerances and thread classes saves the questions a sample raises.
- One-off drawings come from the same certified, heat-traced bar as standard parts.
Heat treatment and coating are done by approved Houston processors, outside our shop. Every lot ships with an EN 10204 3.1 report; certification & traceability.
Order them at the start.
Thread gauging and dimensional inspection
Threads are checked with Go and No-Go ring and plug gauges, and pitch diameter is measured by the three-wire method or on a thread comparator. Heads, flats, lengths and radii are measured with calibrated instruments and, for complex parts, on the CMM.
Is the alloy what the paperwork says?Positive Material Identification (PMI)
A handheld X-ray fluorescence analyser reads the chemistry of the finished part in seconds and matches it to the grade. It confirms that a B7 is chromium-molybdenum steel and not plain carbon, that a B8M has its molybdenum, and that a nickel-alloy stud is the alloy on the certificate. Handheld XRF does not read carbon, so carbon is confirmed from the mill certificate or by spark (OES) analysis.
Is the heat treatment right, and is it soft enough for sour service?Hardness testing
A Rockwell or Brinell indenter is pressed into the part and the indentation measured. Hardness tracks the heat treatment, so it catches an under-tempered lot, and sour-service grades carry a hardness ceiling that every piece must meet.
Any cracks or laps in the surface?Magnetic particle inspection (MPI)
The part is magnetised and dusted with fine iron particles, dry or in a fluorescent suspension. A crack, seam or lap at or just under the surface breaks the magnetic field and the particles gather along it, showing a defect the eye cannot see.
Does it meet the strength table?Tensile testing
The full-size fastener is pulled to failure to prove the load it carries, and a specimen machined from the lot gives tensile strength, 0.2 percent offset yield, elongation and reduction of area. All are compared with the grade's table by diameter.
Jobs we’ve made to drawing.
Common questions.
Can you make a part from a sample, without a drawing?
Yes. Send the part that failed, with whatever you know about its grade and service. We confirm dimensions, threads and grade with you before we cut metal.
Is there a minimum quantity?
No. One-off drawings and short runs are made from the same certified, heat-traced bar as standard parts.
What files can I send?
PDF, DWG, DXF or STEP drawings, images or spreadsheets — attach them to the quote form, up to 5 files and 20 MB.
Do custom parts come with certification?
Yes. Every lot ships with an EN 10204 3.1 material test report traceable to the heat; PMI, Charpy, 3.2 and NACE MR0175 on request.